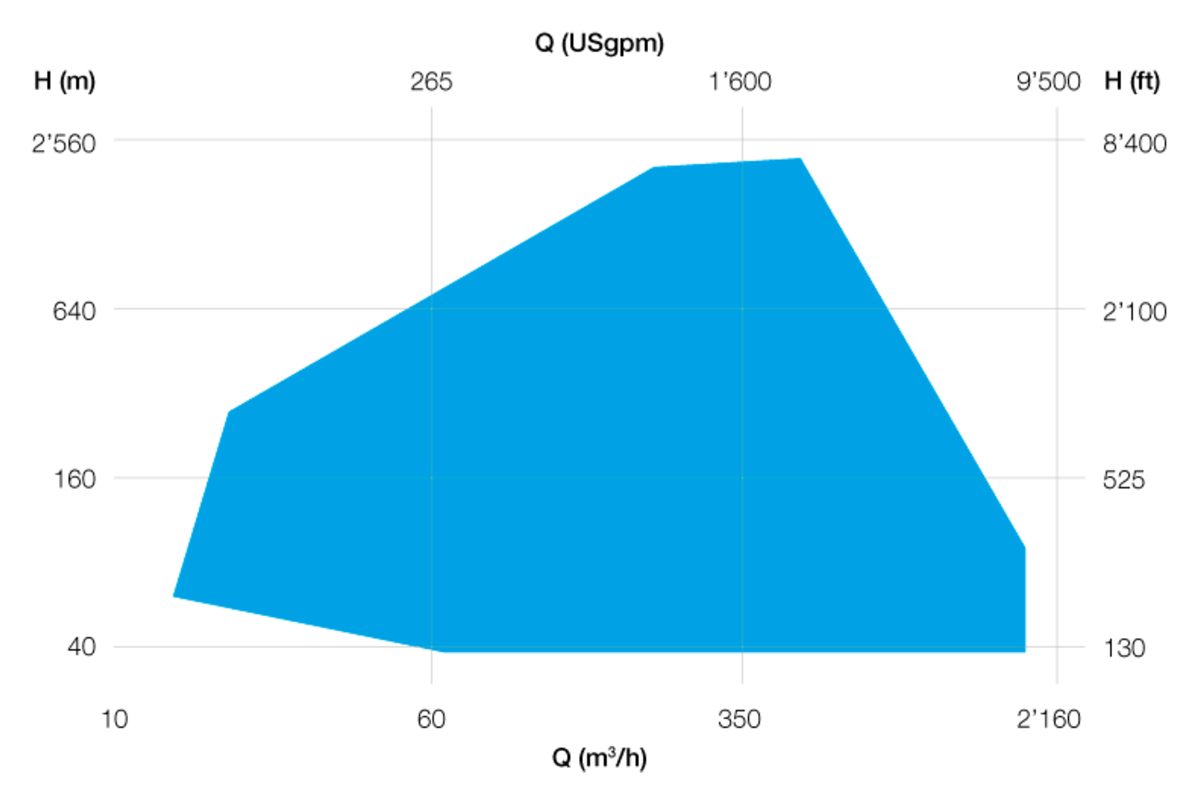
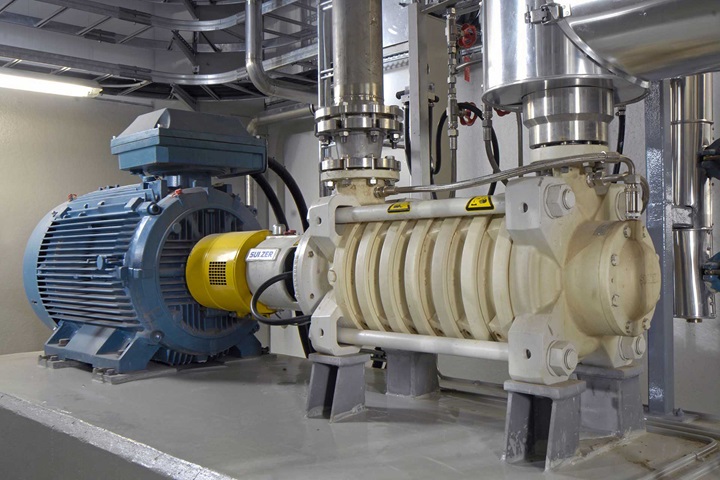
The JVCR pump is an ISO13709 / API610 Type VS6 vertical multistage can pump that is used in situations where Net Positive Suction Head Available (NPSHa) is limited. A wide range of hydraulics, discharge headgear, and pressure ratings may be supplied depending on individual application requirements.
Producers of Liquefied Natural Gas (LNG) can rely on Sulzer’s separation technologies and new injection-mixing devices for desuperheating. Sulzer has also developed pumps for tanker loading and tank farm transfer, which operate reliably at cryogenic temperatures.
We offer broad expertise and experience in gas processing. Our pumps, mixing, and separation technologies are applied in process gas scrubbing, gas drying, gas purification, gas fractionation, condensate stabilization, and gas-liquid separation. We also offer services for rotating equipment.
Maximize efficiency and durability in copper applications, while reducing energy costs and water consumption. With an advanced selection of materials for a comprehensive portfolio, Sulzer ensures reliable performance at minimized downtime, even in demanding environments.
Sulzer has a deep knowledge in wastewater treatment, and with our wide product portfolio we can now offer energy-efficient and reliable solutions for your water collection, neutralization, flocculation, sedimentation, cooling, aeration, sludge storage, digestion, and dewatering processes.
We support complex industrial processes with tailored water and wastewater treatment solutions by combining process understanding, proven technologies, and global experience across demanding industries.
Sulzer’s extensive product portfolio to maximize the performance and reliability of your solid organic fuel biomass power plant, solid industrial or municipal waste fuel biomass power plant, and liquid or gaseous organic fuel biomass power plant processes.
Discover Sulzer's best solution for LNG pumping
To view the integration, please enable Targeting Cookies.