HSV high-speed vacuum pump (Available in Europe, Brazil, the USA, and Canada only. Contact us for other regions.)
Achieve superior vacuum performance with unmatched efficiency and reliability
The Sulzer HSV high-speed vacuum pump series delivers mission-critical, high-capacity vacuum for advanced industries. Engineered for powerful performance, exceptional stability, and a significantly lower total cost of ownership.
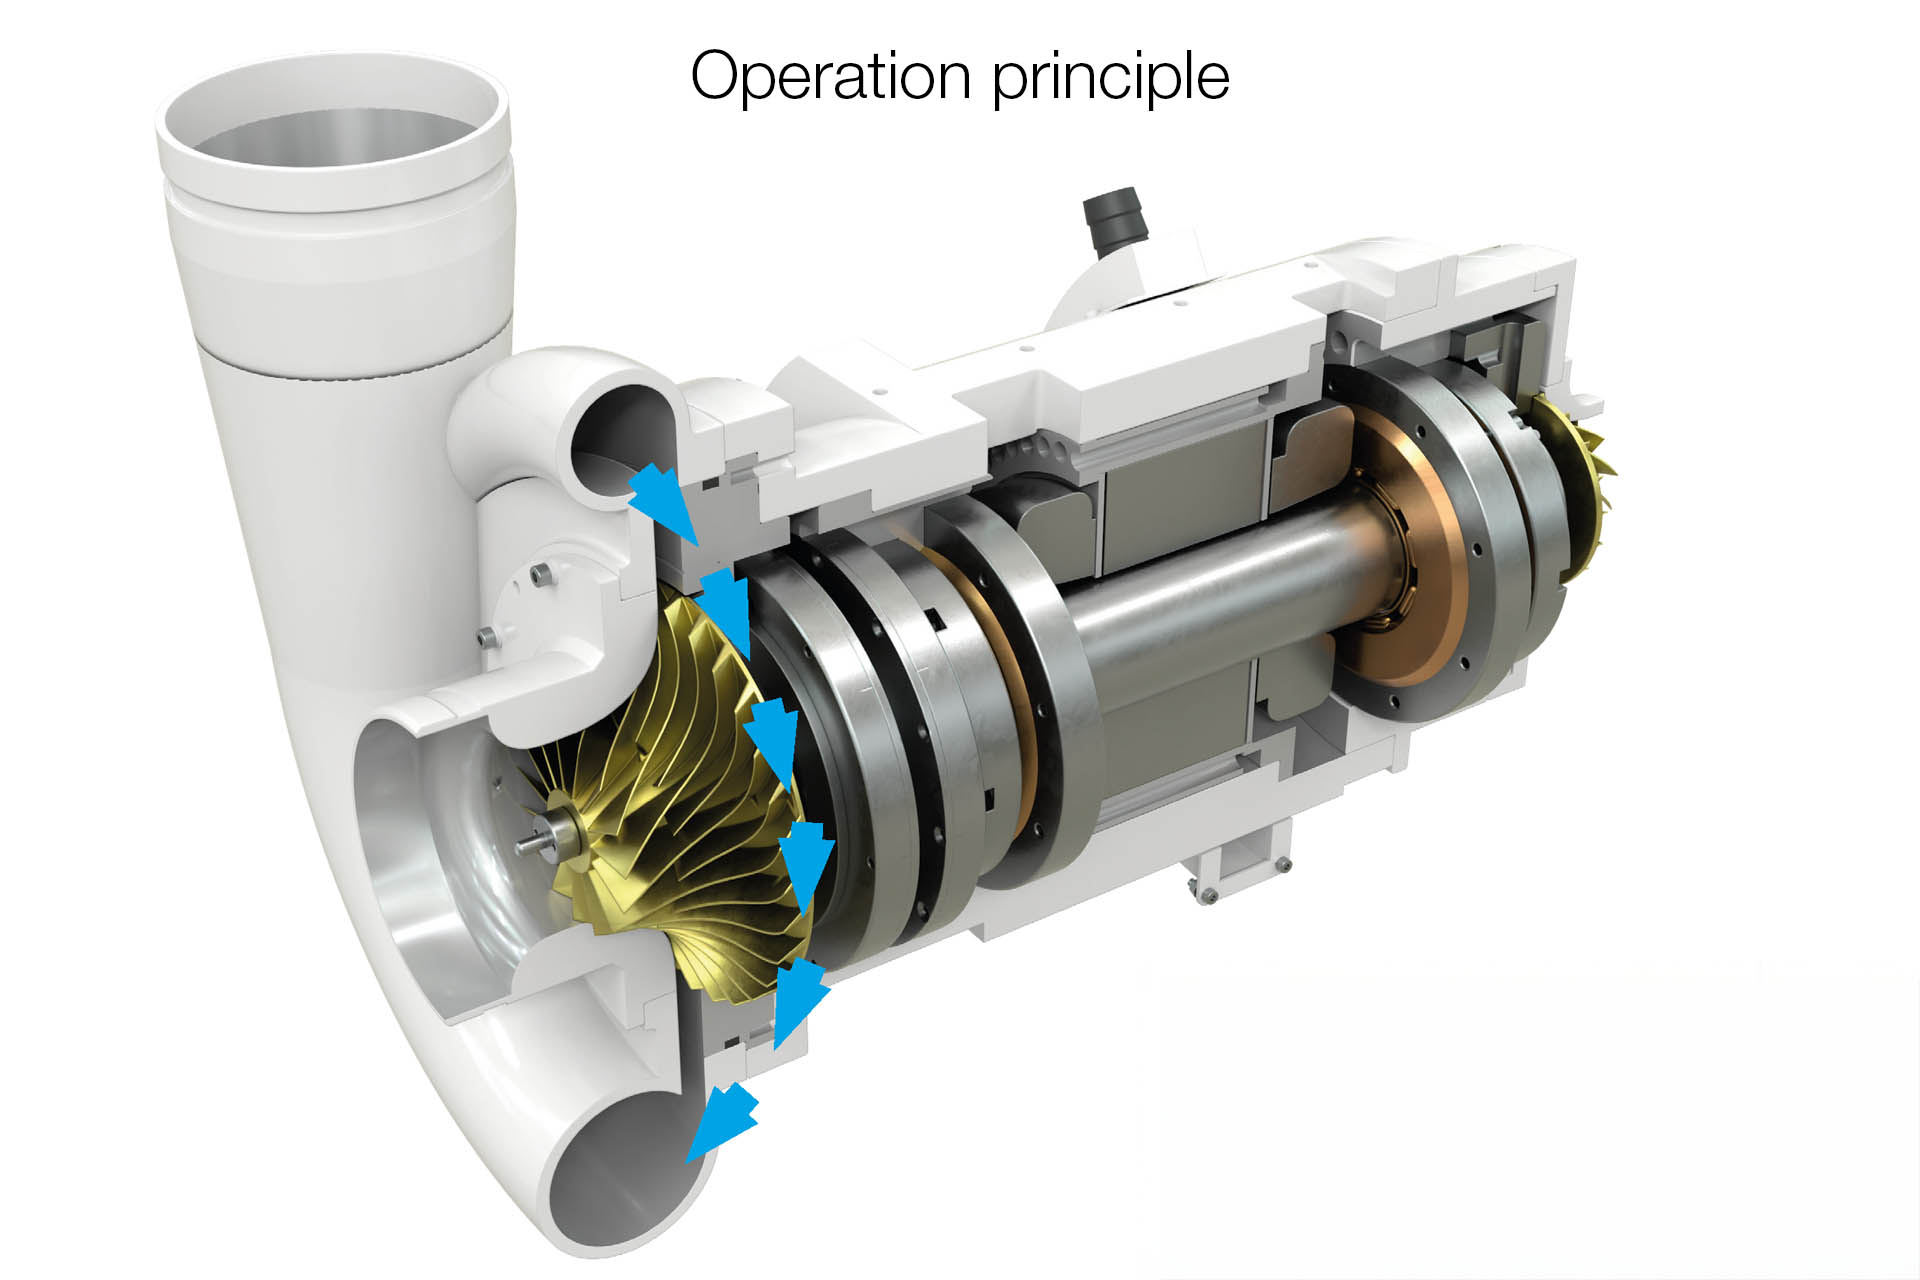
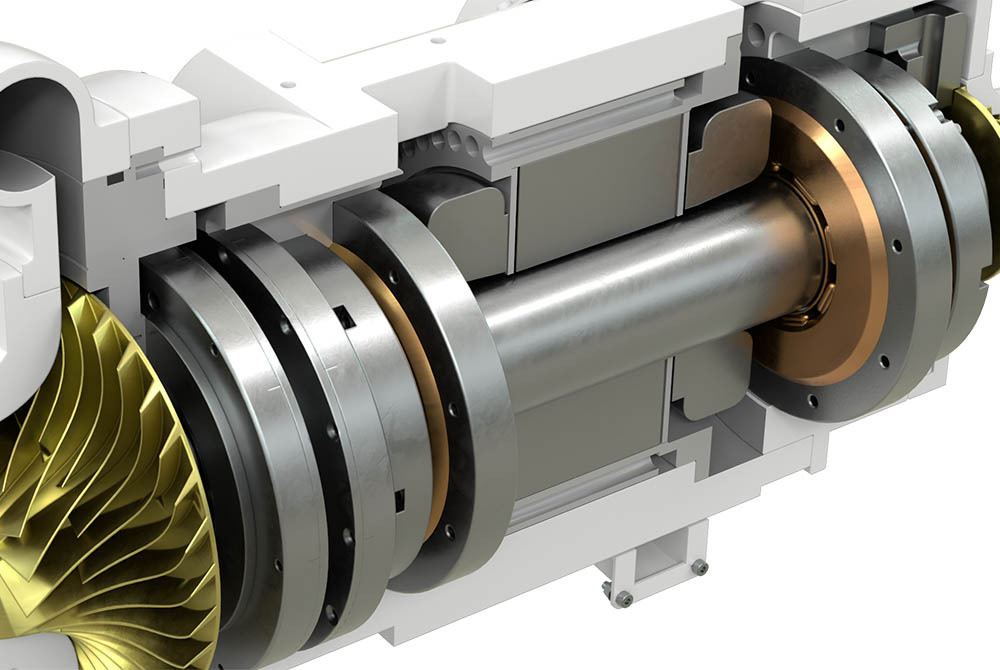
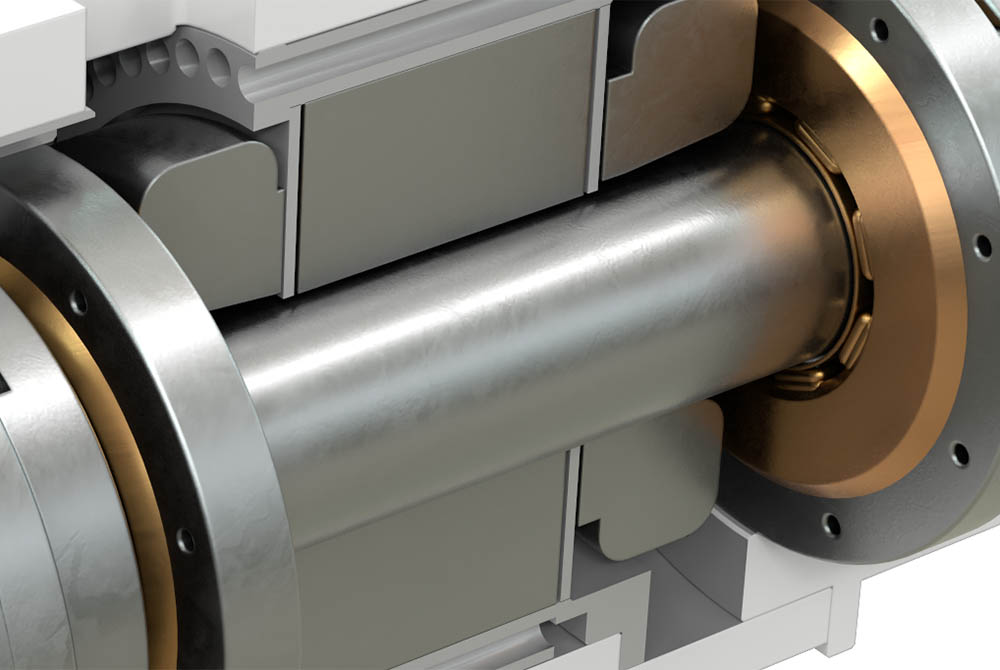
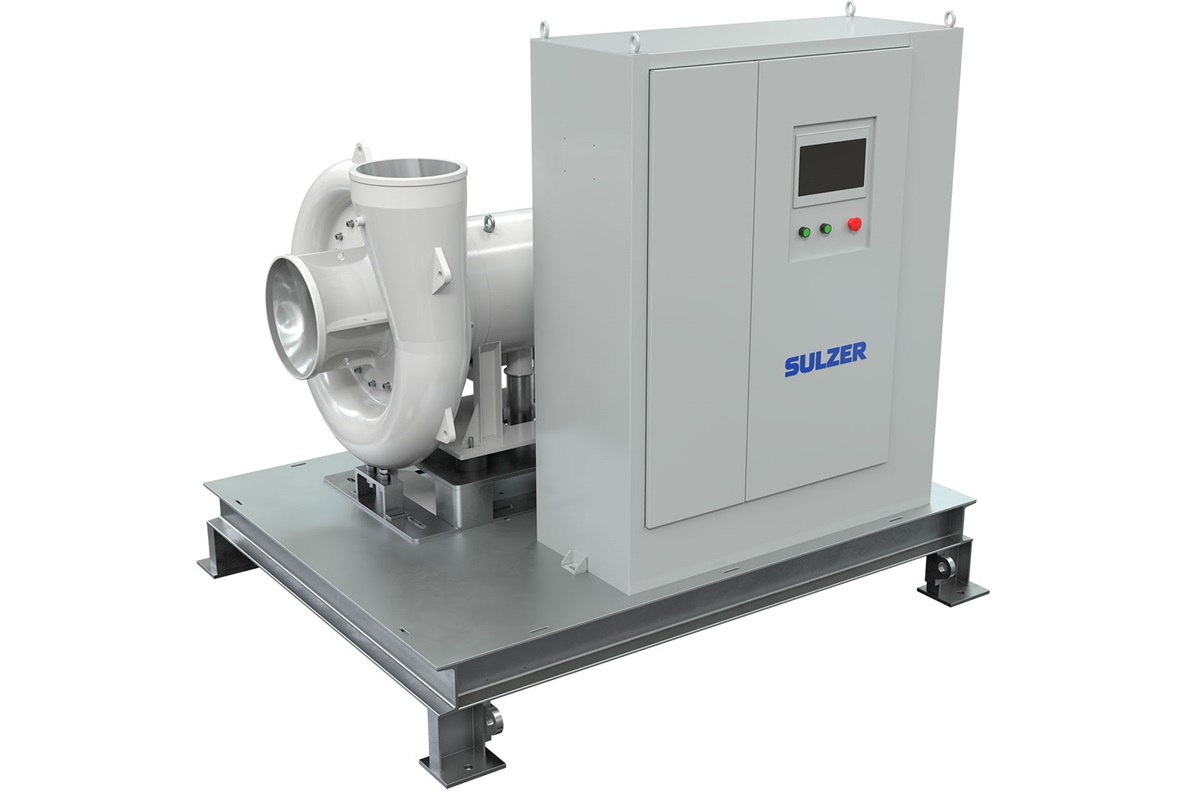
Frictionless, oil-free active magnetic levitation ensures extended lifespan, minimal maintenance, and ultra-low vibration for sensitive processes.
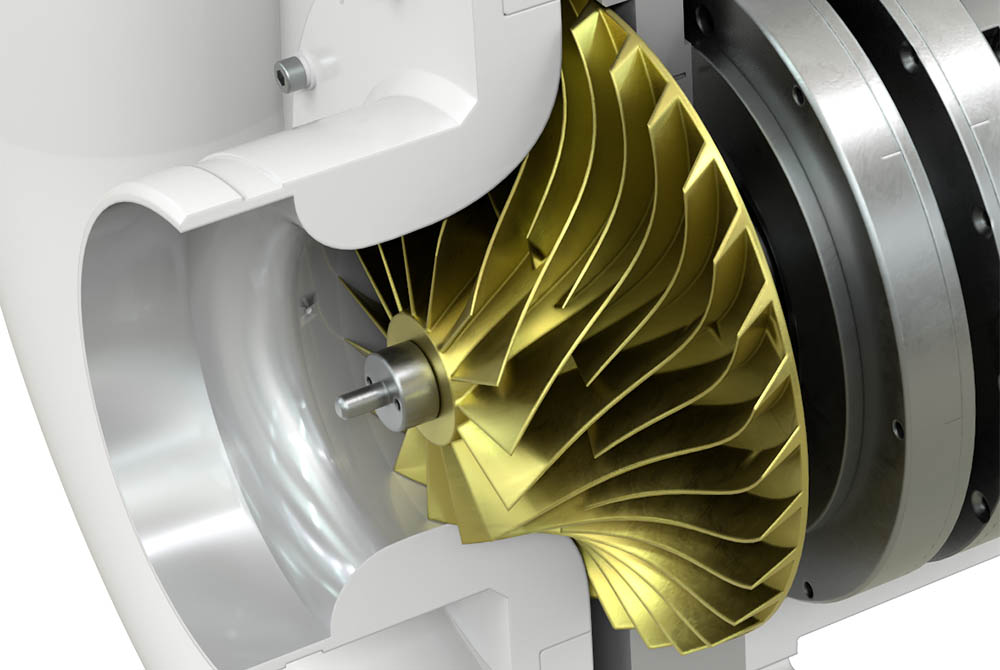
High-efficiency impeller design, precision-machined from high-strength alloys for rapid pump-down and superior durability.
High-speed permanent magnet motor (up to 60’000 rpm) delivers energy-efficient, friction-free direct drive power with high-temperature resistance.
Advanced control unit with high-frequency vector inverter and intelligent algorithms provide precise speed control, energy savings, and power outage protection.
Integrated diagnostics and safeguards offer comprehensive monitoring and built-in protection for enhanced reliability and remote management.
Robust, actively cooled construction ensures durability, easy integration, and extended component life.
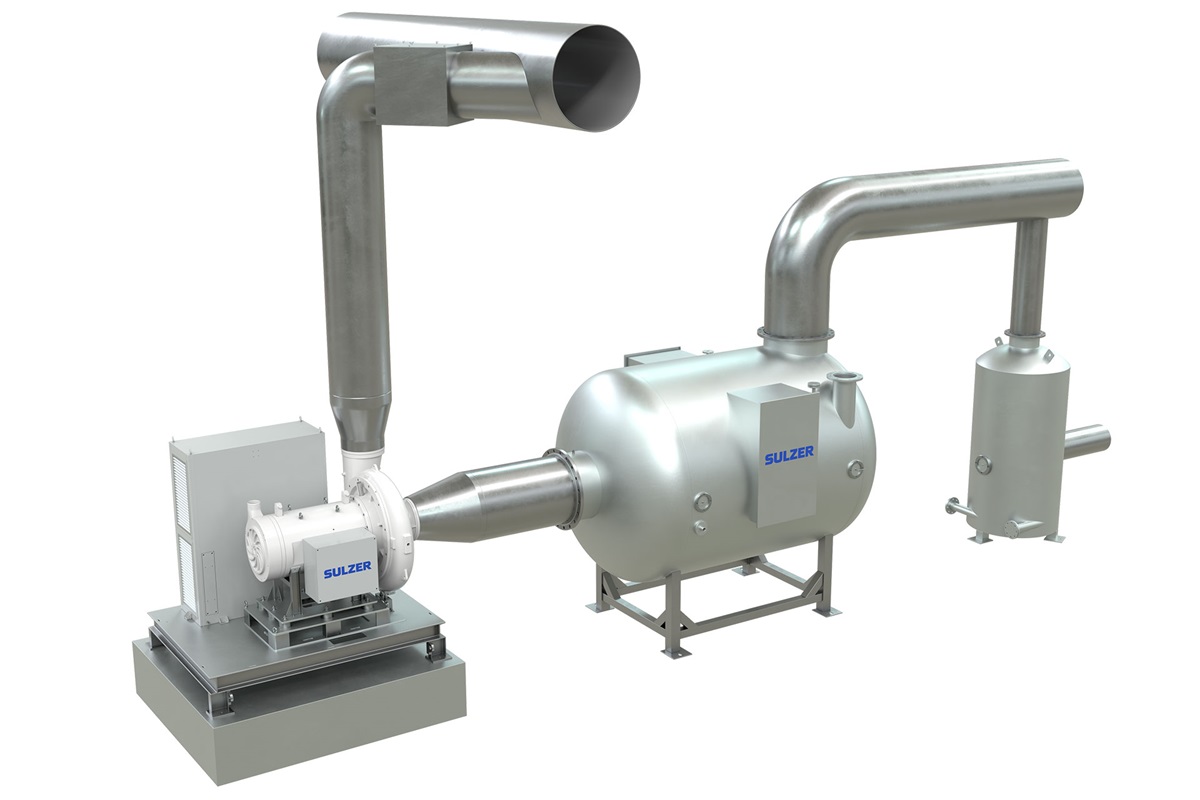
304 SS steam-water separator with demister/spray and auto-level control for effective impurity removal.
Optional vent valve for automated safe process venting.
HSV vacuum pumping system and steam-water separator
Sulzer is the world leader in innovative, reliable, and proven pumping, agitation and mixing solutions for the pulp and paper industry. Our deep process and application knowledge is based on long-term close co-operation with the producers, machinery suppliers and engineering companies.
Our solutions for the chemical processing industry include pumping, separation and mixing, as well as services for rotating equipment and infrastructure. We offer experience in classical chemical, plastic, and pharmaceutical production as well as in processing renewable materials.
Our pumps, mixers and agitators provide durability and reliability for fertilizers production as well as for corrosive and abrasive liquids and high gas content. Our specific industry experience also includes separation processes and servicing of pumps, compressors, turbines, and motors.
Biofuels from renewable sources show great potential as sustainable transportation fuel. Based on our experience in demanding processes, we work with customers to develop advanced pumping, mixing, and distillation solutions for the production of biofuels, from pilot to commercial-scale installations.
Food and beverage production relies on our pumping and mixing solutions. Special pumps and agitators have been developed for sugar, starch, and sweetener production. Separation equipment is often used in beverage manufacturing and our process technologies support purification and concentration.
You can rely on our high-performance pumps for efficient operations of fossil-fired, nuclear, and renewable power generation. Our maintenance and repair services for turbines, pumps, and generators ensure continuous operations.
Sulzer’s pumping and mixing solutions for the metal industry are designed for corrosive and abrasive liquids. We offer expertise e.g. for the production of aluminum, copper, nickel, zinc, and precious metals.
Whether on the surface or underground, the conditions in mines are harsh. Besides the mud, slurry, stones, and rocks, there are large volumes of water to remove in order to keep production moving.
Our dewatering pumps are rugged and ready, taking on the toughest drainage and sludge removal.